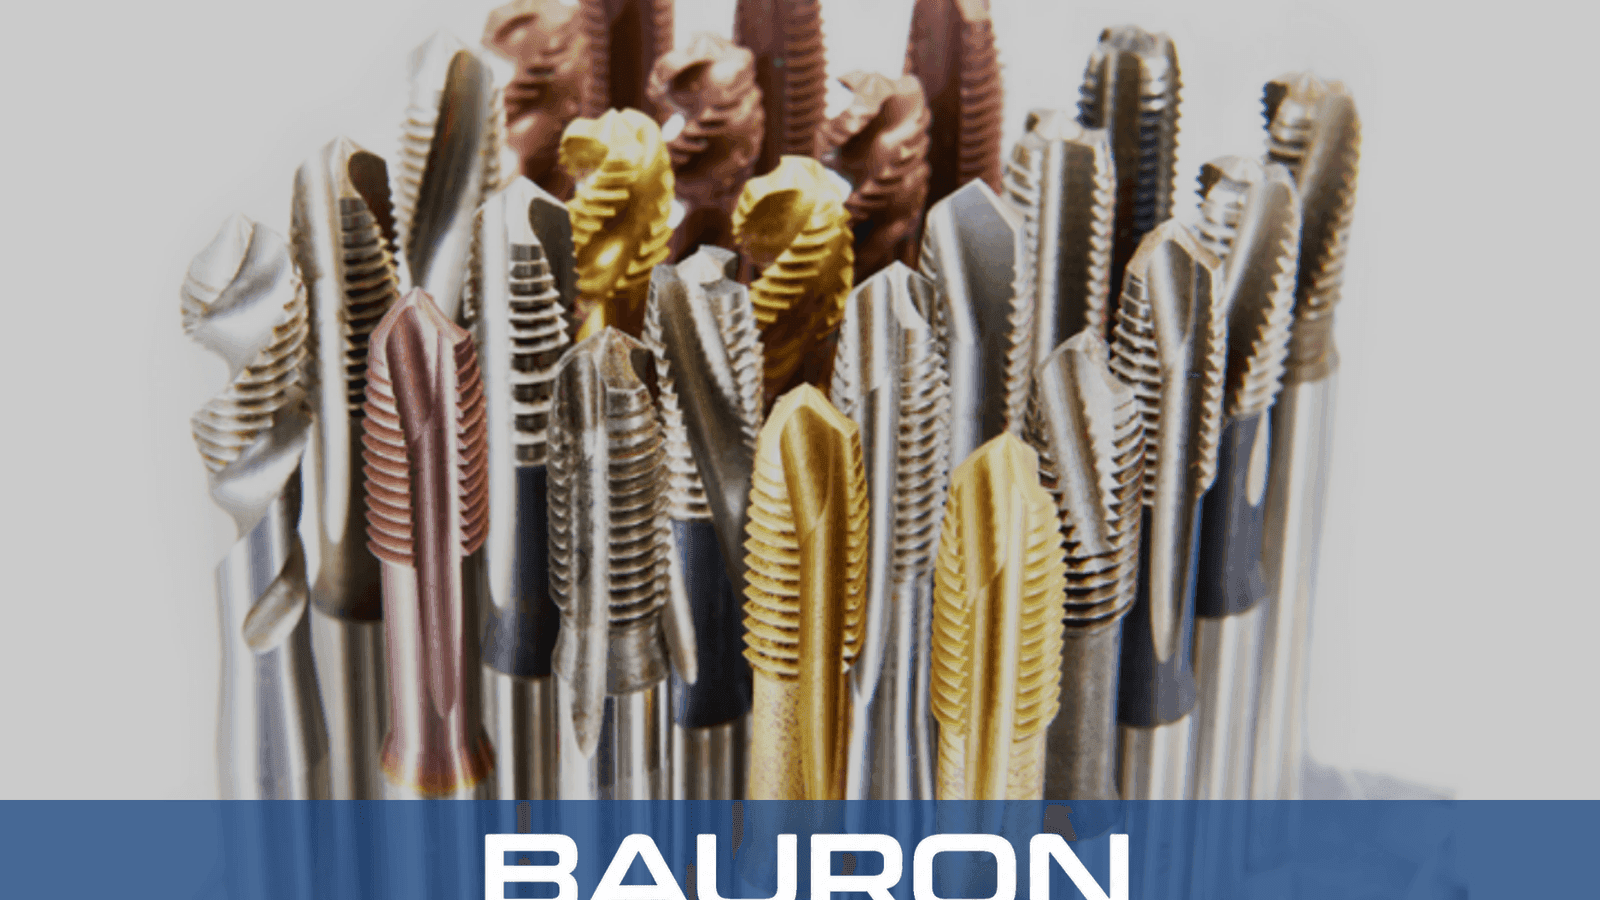
Helical Lift
Angled flutes direct continuous chips upward as the tap rotates and advances.
Spiral flute taps are internal thread-cutting tools designed primarily for blind holes. Their continuous helical flutes shear material and transport chips back toward the hole entrance rather than ahead of the tool into the cavity.
Angled flutes direct continuous chips upward as the tap rotates and advances.
Chips travel toward the entrance instead of accumulating at the blind-hole floor.
Helical cutting edges slice ductile materials while forming the internal thread profile.
Removing chips from the cavity preserves space below the tap for controlled thread depth.
Helical flutes draw chips out of blind holes and can reduce compression at the cavity floor.
Application-specific helix forms support controlled automated tapping cycles.
Helical edges can produce clean thread surfaces when geometry and cutting conditions match the material.
Helix selection balances chip transport, edge strength, and flute space for the workpiece material.
Modified bottoming and plug chamfers provide different balances of starting guidance and blind-hole thread reach.
| Specification | Range / Details |
|---|---|
| Diameter Range | #0 to 2"+; metric M1.6 to M50+ available |
| Helix Angle | 15° slow helix to 45°+ fast helix |
| Chamfer Profile | Modified bottoming, 2 to 3 threads; or plug chamfer, 3 to 5 threads |
| Thread Forms | UNC, UNF, metric, NPT, and custom pitch profiles |
| Shank Type | Standard square drive or straight cylindrical |
| Tolerance | GH and H-class precision options |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS-E (Cobalt) | Stainless steel, alloy steel, and titanium. | Hot hardness helps retain the cutting edge in tough, ductile materials. |
| Solid Carbide | High-hardness materials and stable production setups. | Rigidity and wear resistance support high-speed machine tapping when alignment is controlled. |
| TiAlN / CrN Coating | Stainless steel, selected aluminum applications, and dry or limited-lubrication processes. | Lower friction can reduce material buildup, subject to coating-workpiece compatibility. |
Cobalt HSS-E combines toughness and hot hardness, solid carbide adds rigidity and wear resistance in stable setups, and TiAlN or CrN coatings can lower friction when matched to the workpiece.
Use rigid tapping cycles and controlled chip evacuation for blind-hole threads.
Mount taps in live-tool or axial turrets to thread blind holes in turned parts.
Provide repeatable forward and reverse motion in dedicated production equipment.
Cuts internal threads in non-through holes while directing chips toward the entrance.
Handles materials such as stainless steel, aluminum, and structural steel that can form continuous chips.
Application-matched geometry can traverse cross-holes or keyways in blind cavities with reduced chip congestion.
Integrates with rigid machine-tapping cycles where speed, feed, coolant, and reversal are controlled.
Choose spiral flute geometry for blind holes because it draws chips toward the entrance. Spiral point taps push chips forward and are generally intended for through-holes.
Higher helix angles around 40° to 45° can aid evacuation of long chips from softer ductile materials. Lower angles around 15° to 30° provide a stronger edge for tougher materials. Confirm the selection against the specific alloy and process.
Manual use is possible in some cases but is generally less suitable than machine control because the deep flutes reduce core section and hand alignment can introduce side loading.
Possible causes include insufficient flute capacity, an unsuitable helix angle, inadequate lubrication or coolant delivery, an undersized pilot hole, excessive depth, or chip congestion.
Application-specific options can include custom helix angles, pitches, chamfers, coolant-through channels, shank dimensions, substrates, and coatings.
Bauron provides design and engineering support for custom thread geometry, helix angle, flute capacity, coolant delivery, substrate, and coating selection. Share the blind-hole dimensions, workpiece material, and cycle requirements for technical review.
Talk to Engineering