Segmented Chip Creation
Interrupted cutting edges split wide metal shavings into small chips.
A chipbreaker end mill addresses heavy stock evacuation in tough, ductile materials. Ground notches or offset serrations along the peripheral edges divide continuous metal ribbons into manageable chips before they wrap around the tool or pack into deep pockets.
Interrupted cutting edges split wide metal shavings into small chips.
A smaller chip-to-tool contact area lowers cutting resistance and heat generation.
Small chips clear from deep flutes and narrow slots with coolant or air blast.
Chip control supports greater axial depths and faster table feeds while reducing jamming risk.
Supports aggressive feeds and axial depths to reduce roughing cycle time.
Chopped shavings clear flutes more readily and reduce breakage risk in deep pockets.
The interrupted-tooth design reduces cutting forces on the spindle.
Staggered serrations disrupt cutting frequencies to reduce vibration on deep cuts.
Reduced friction and heat buildup help protect cutting flutes from thermal wear.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/4" to 1-1/2"+; metric 6 mm to 32 mm+ available |
| Profile Style | Fine pitch for tough alloys and steels; coarse pitch for aluminum and soft metals |
| Flute Count | 3, 4, 5, or 6 flutes |
| End Profiles | Square end, chamfered, or corner radius (bull nose) |
| Shank Style | Straight cylindrical or Weldon-flat shank |
| Operation Type | High-efficiency roughing, deep slotting, and trochoidal milling |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Solid Carbide | Stainless steel, titanium, hardened tool steels, and cast iron. | Structural stiffness resists flex during heavy roughing passes. |
| AlTiN / TiAlN Coating | Tough alloy steels, stainless steel, and dry high-heat milling. | Thermal hardness protects serrated edges from heat-related degradation. |
| nACo / DLC Coating | Aluminum alloys, brass, and non-ferrous soft metals. | Helps prevent soft material from galling or welding inside chipbreaker notches. |
Solid carbide provides roughing stiffness, AlTiN or TiAlN protects edges in ferrous high-heat work, and nACo or DLC helps control galling in non-ferrous materials.
Run dynamic roughing and deep-slotting operations.
Run heavy axial cuts in large structural steel forgings.
Use live-tool turrets for cross-milling and deep keyway roughing.
Removes volumes of material from deep internal cavities and channels.
Runs dynamic milling paths with full axial engagement in tough alloys.
Controls bird-nesting when roughing ductile stainless steel, aluminum, and low-carbon steel.
Removes stock from forged titanium and aluminum airframe components.
Traditional roughers use coarse waveform teeth that leave a wavy wall. A chipbreaker uses offset notches in otherwise smooth flutes, breaking chips while leaving a smoother surface that may need only a light finishing pass.
Ductile materials create continuous ribbons that can wrap around the spindle or clog flutes. Chipbreaker geometry divides those ribbons into smaller chips.
They produce a smoother finish than traditional roughers, but the micro-notches can leave line marks. Use a dedicated finishing end mill for high-precision or polished surface requirements.
Coarse-pitch tools have larger notches for soft materials such as aluminum. Fine-pitch tools use smaller, closely spaced notches for stainless steel, titanium, and hardened alloy steels.
Bauron can engineer notch geometries, variable helix angles, corner radii, and TiAlN or nACo coatings for specific manufacturing requirements.
Bauron provides design and engineering support for tooling requirements. The engineering team works with customers on custom geometries, specialized coatings, and complex machining challenges.
Talk to Engineering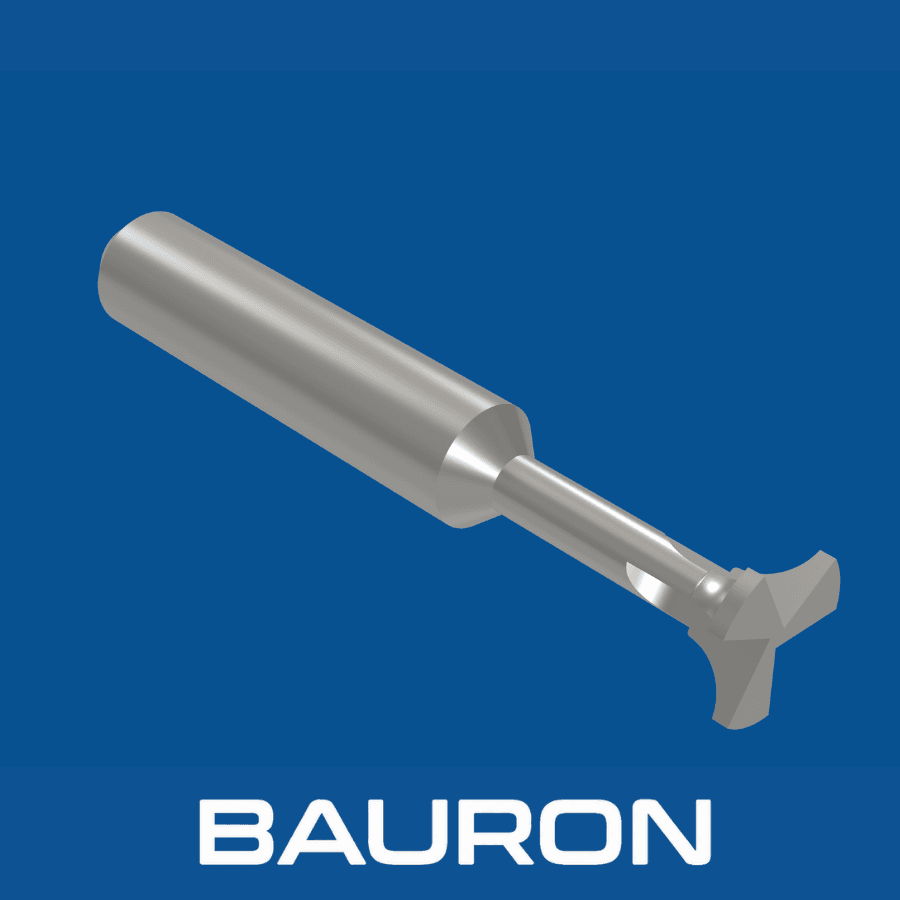
A back corner rounding end mill uses a reverse-concave profile to deburr and radius back-side hole edges and underside workpiece corners in a single setup.
View Product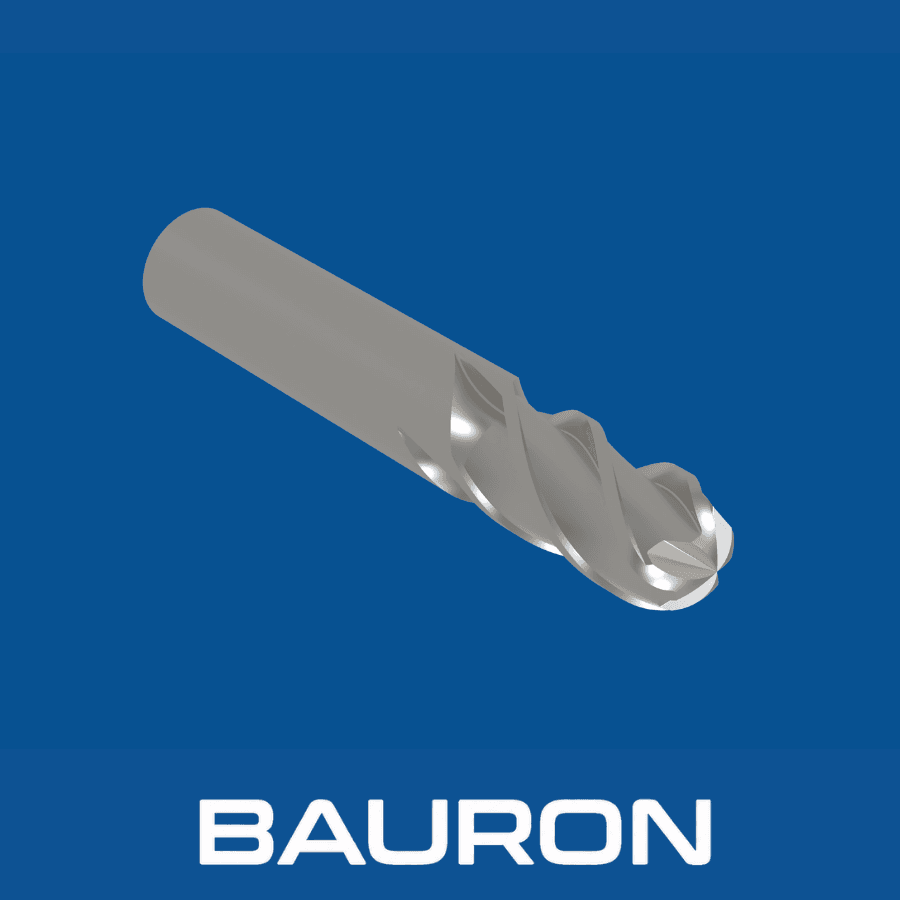
A ball nose end mill is a form-milling tool with a hemispherical cutting tip for 3D contouring, die sinking, and machining complex curved surfaces.
View Product
A pointed chamfer cutter is an angled cutting tool with a sharp tip for beveling hole edges, deburring corners, countersinking, and engraving fine details.
View Product
A tipped-off chamfer cutter is an angular milling tool with a truncated flat end that increases tip strength for edge beveling, deburring, and countersinking.
View ProductWork with Bauron's engineering team to develop a cutting tool tailored to your application, material and machining requirements.